- English
- French
- German
- Portuguese
- Spanish
- Russian
- Japanese
- Korean
- Arabic
- Greek
- German
- Turkish
- Italian
- Danish
- Romanian
- Indonesian
- Czech
- Afrikaans
- Swedish
- Polish
- Basque
- Catalan
- Esperanto
- Hindi
- Lao
- Albanian
- Amharic
- Armenian
- Azerbaijani
- Belarusian
- Bengali
- Bosnian
- Bulgarian
- Cebuano
- Chichewa
- Corsican
- Croatian
- Dutch
- Estonian
- Filipino
- Finnish
- Frisian
- Galician
- Georgian
- Gujarati
- Haitian
- Hausa
- Hawaiian
- Hebrew
- Hmong
- Hungarian
- Icelandic
- Igbo
- Javanese
- Kannada
- Kazakh
- Khmer
- Kurdish
- Kyrgyz
- Latin
- Latvian
- Lithuanian
- Luxembou..
- Macedonian
- Malagasy
- Malay
- Malayalam
- Maltese
- Maori
- Marathi
- Mongolian
- Burmese
- Nepali
- Norwegian
- Pashto
- Persian
- Punjabi
- Serbian
- Sesotho
- Sinhala
- Slovak
- Slovenian
- Somali
- Samoan
- Scots Gaelic
- Shona
- Sindhi
- Sundanese
- Swahili
- Tajik
- Tamil
- Telugu
- Thai
- Ukrainian
- Urdu
- Uzbek
- Vietnamese
- Welsh
- Xhosa
- Yiddish
- Yoruba
- Zulu
Mining Equipment Steel Workshop for Heavy-Duty Machinery
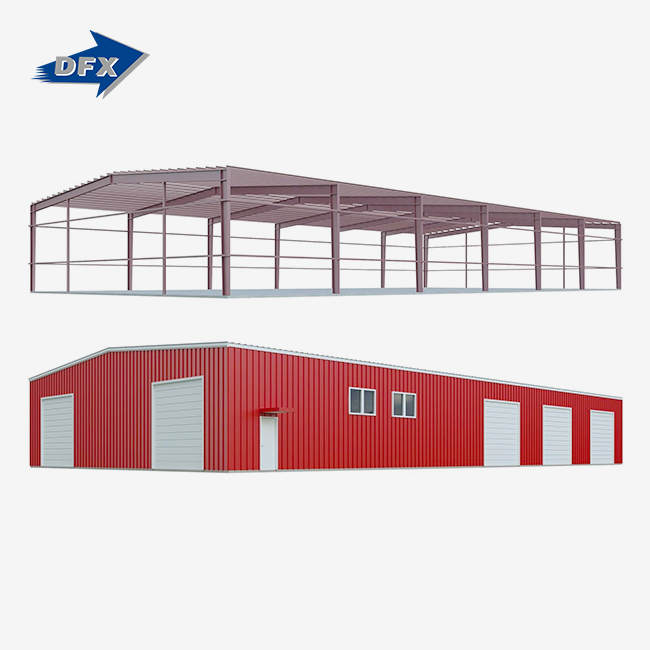
A mining equipment steel workshop is a purpose-built industrial facility designed to house, maintain, and fabricate massive mining machinery — from gyratory crushers and ball mills to 400-ton haul trucks. Unlike standard commercial buildings, these structures carry extreme dynamic loads from overhead cranes, resist corrosive atmospheres common at mine sites, and provide wide clear spans for unobstructed equipment movement. Built with high-strength structural steel frames and engineered for decades of continuous operation, a well-designed heavy-duty steel workshop is the operational backbone of any serious mining or mineral processing project.

Understanding the Essential Types of Steel Workshop Equipment for Mining Machinery
Each business that works well needs to have the right tools and a clear idea of what those tools need to do every day.
Cutting Technologies for Heavy Steel Fabrication
Plasma cutting, laser cutting, and oxy-fuel cutting are the three main ways that heavy-duty shops cut things. Plasma cutting is a common way to make mining parts because it works well with thick low-alloy steel plates. Laser devices can make thinner shapes with tighter tolerances. Oxygen fuel is still the best choice for parts that are thicker than 100 mm. The type of steel (Q355B or ASTM A572 Gr 50 is common in mining buildings) and the quality of the edge that needs to be welded later determine the best way.
Welding Equipment: MIG, TIG, and Stick Welders
MIG welding is the most common method used in production settings because it is fast and can be used on steel of different sizes. TIG welding is best for making precise joints on structural links where the quality of the weld is checked against AWS D1.1 or EN 1090 standards. Stick welding can still be used for fixes in the field and in places where power isn't always available. Full-penetration butt welds on crane runway beams and column brackets are tested with ultrasonic waves to make sure there are no interior flaws. This is an important quality step that can't be skipped.
Safety Practices and Maintenance Protocols
In a mining equipment steel workshop, workers must wear arc-flash face masks, cut-resistant gloves, steel-toed boots, and respiratory protection while cutting and coating. Welding machines, overhead cranes, and cutting tables need regular maintenance to avoid unplanned downtime. The U.S. Bureau of Labor Statistics says that fabrication plants with recorded preventive maintenance plans have 23% fewer equipment-related work stops each year. Regular checks and testing records also help get ready for an ISO 9001 audit.
Optimizing Steel Workshop Layout for Heavy-Duty Mining Equipment Fabrication
Every day, a bad plan costs money. Things move farther than they need to, cranes bump into each other, and workers have to wait. All of that can be avoided if the floor plan is done right from the start.
Zoning for Workflow Efficiency
The most efficient workshop plans split the tasks of cutting, welding, and putting things together into clear areas with easy access between them. The raw steel goes from the cutting zone to the welding bays to the assembly area in a straight line, so there is no need to go backward. For mining shops that work with parts that weigh 20 tons or more, the crane must cover all three zones without any dead spots.
Smart Storage and Material Handling Systems
Magnetic lifting equipment and vertical steel rack systems clear up the floor and make it easier to get to structural shapes and plate stock. By cutting down on the time it takes to look for and move things, a well-organized workshop can handle 30% more tonnage each year. In workshops that work on high-end mining equipment, overhead bridge cranes with ratings of 50T to 200T are common. The runways of these cranes must line up perfectly with the column spacing in the building frame.
Real-World Layout Case Study
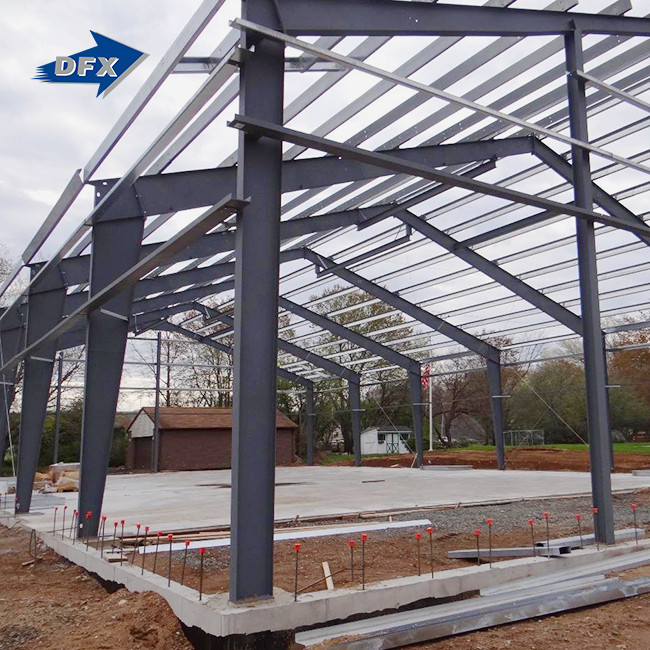
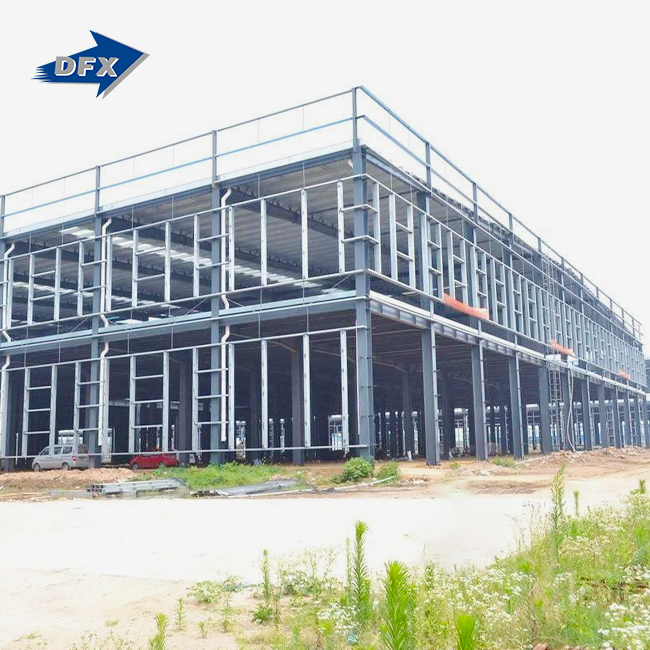
A mineral processing facility in Western Australia changed the layout of its maintenance workshop by adding a dedicated crane bay with a 9-meter eave height and separating its MRO zone from its fabrication shop. The average time it took to turn over equipment was cut by 40%. That column-free layout was possible with wide-span steel structures that had clear internal room. These structures were similar in idea to the large-span buildings made by Director Steel.
Comparing Manual and Automated Equipment for Mining Steel Workshops
One of the most important investment choices a buying manager has to make is whether to buy manual or automatic tools. There are real trade-offs with both choices that should be carefully considered.
Cost, Precision, and Productivity
In a mining equipment steel workshop, manual equipment costs less to buy at first, but it needs skilled workers, and the quality of the welds can vary more. Automated welding systems and CNC plasma tables cut the cost of labor by up to 45% per unit on high-volume runs and keep the tolerances for size within ±1 mm, which is the same level of accuracy used in Director Steel's plant pre-assembly process. Based on normal production rates, automation pays for itself in 18 to 36 months in workshops that make mine parts that are used over and over again.
Here are the main differences that you should think about when making your purchase decision:
- Manual tools suit low-volume, complex, or site-based work where flexibility matters more than throughput speed. They require less capital and allow skilled welders to adapt to non-standard geometries common in mining repair jobs.
- Automated systems deliver consistent output quality, reduce operator fatigue-related errors, and generate data logs that support traceability requirements under ISO 9001 audits.
These differences have a direct effect on the long-term costs of running the business, planning the workforce, and the structural quality of final parts. By matching the type of tool to the way you actually make things, you can avoid both under-investment and over-capitalization.
Energy Consumption and Sustainability
Up to 30% less energy is used by automated inverter-based welding systems than by older transformer units with the same output. As mining companies are required to report on environmental, social, and governance issues more often, using less energy to make steel is a measurable indicator of sustainability. It's easier for buying teams to follow audit rules when equipment providers give them energy certificates and performance data.
Brand Evaluation Criteria
When looking at different providers and types of equipment, it's important to make sure that the guarantee terms are clear, that there are reliable after-sales support networks in your area, and that spare parts are available for operations that take place at a remote spot. Manufacturers with ISO 9001 certification and CE markings provide a quality standard that can be tracked. This protects procurement teams when auditors look at supplier qualification records.
Procurement Guide: How to Source and Purchase Steel Workshop Equipment for Mining Industry
The same kind of deliberate thinking goes into getting the building itself, not just the tools inside.
Supplier Certification and Quality Verification
Check to see if the company that sells steel structures has ISO 9001 approval and that their structural steel goods are marked with the CE mark. Ask for Mill Test Certificates (MTC) that state the steel's yield strength and impact toughness meet the design requirements. MTC paperwork is needed at the very least for mining uses that use Q355B/C/D or ASTM A572 Gr 50. Director Steel was established in 2011 and has more than 12 years of experience in fabrication. All of their structures are made using quality systems that are ISO 9001 and CE certified and can be fully tracked through the MTC system.
Logistics for Oversized Components
In mining workshops, columns that are longer than 12 meters and crane beams that are longer than 15 meters are common. These members need open-top containers or flat-rack shipping, and the logistics plan needs to take into account the size limits for port clearance and any restrictions on road transport at the destination. Director Steel's bolted link design makes sure that the right-sized parts are used for loading containers, and thorough 3D installation plans make it possible for local teams to build the structure without having to weld it on-site.
Delivery Timeline and Custom Orders
For a mining equipment steel workshop, it usually takes 25–49 days from the time the plan is approved to the time the steel structures are sent out of the mill for heavy-duty mining workshops. This schedule lets us make custom-sized crane runway beams, stronger column brackets for 50T to 200T cranes, and corrosion protection systems that meet ISO 12944 C4/C5 standards. Critical-path delays on site can be avoided by making sure of the delivery plan before the project starts moving forward.
Leveraging Latest Technologies and Automation in Mining Equipment Steel Workshops
Steel fabrication is going toward output that is tied to data, and mining workshops that use these tools get real benefits in how they run their businesses.
Automated Welding and CNC Fabrication
Director Steel has six automatic welded H-beam production lines that can make up to 20,000 tons of welded H-beams and columns every year. At this level of automation, measurements are accurate, welds are consistent, and production can be tracked in a way that isn't possible with manual fabrication on a large scale. When purchasing managers choose structural steel for workshops on mine sites, automated manufacturing cuts down on problems with field fit-up and the cost of repairs.
IoT and Predictive Maintenance
IoT-connected sensors built into cranes and structural tracking points let maintenance teams keep track of load cycles, spot signs of wear and tear, and plan repairs before they fail. McKinsey & Company says that predictive maintenance plans in factories cut down on unexpected downtime by 30–50% and maintenance costs by 10–25%. When mining companies work around the clock, these numbers directly translate into operational savings.
Eco-Friendly Production and Surface Treatment
When used on steel parts in a mine workplace, modern anti-corrosion systems like hot-dip galvanizing above 85 microns, an epoxy zinc-rich primer, and an intermediate coat of micaceous iron oxide can make the structure last longer than 50 years in C5-M classified environments. If you choose a supplier that puts these coatings on in a controlled factory setting instead of on-site, the chance of failure and the cost of long-term upkeep will be lower.
Conclusion
To make a solid mining equipment steel workshop for mining tools, you need to do more than just pick the cheapest steel frame. The building has to be strong enough to hold dynamic crane loads, able to handle corrosive environments, and have enough clear-span room for heavy machines. Long-term performance is affected by all decisions, from choosing the right materials and finishing the surface to planning the layout and making sure the supplier is qualified. Director Steel makes steel structures that are ISO 9001 and CE-certified. These structures have welded H-section frames in Q235/Q355, fixed joints, and full design-to-delivery service. They are made for tough industrial uses like these.
FAQ
Q1: What structural steel grade is recommended for a mining workshop with heavy overhead cranes?
Q355B/C/D or ASTM A572 Gr 50 are standard grades for workshops supporting crane runway beams rated from 50T to 200T. These grades provide the yield strength and impact toughness needed for dynamic loading conditions.
Q2: How long does anti-corrosion coating last in a mining environment?
A properly applied C5-M grade system — epoxy zinc-rich primer plus polyurethane topcoat, or hot-dip galvanizing above 85 microns — provides a structural lifespan exceeding 50 years in acidic or saline atmospheres.
Q3: What is the typical delivery lead time for a custom mining workshop structure?
Made-to-order structures carry a lead time of 25–49 days from design confirmation to factory dispatch, depending on span width, crane capacity, and corrosion protection requirements.
Q4: Can the building design support multiple bridge cranes?
Yes. Reinforced bracket systems and stepped columns allow the structure to carry multiple bridge cranes simultaneously, with each runway beam calculated for specific dynamic wheel loads and braking forces.
Get Your Mining Workshop Quote from Director Steel Today
Director Steel has been supplying heavy-duty steel structures to mining and industry projects in six countries since 2011. We are a reliable mining equipment steel workshop maker with ISO 9001 and CE certification. In 25–49 days, we can deliver custom-designed structures with welded H-section frames, full installation support, and C5-M corrosion protection. A full technical plan will be sent to you within 48 hours if you email your project drawings or basic measurements to jason@bigdirector.com.
References
1. American Institute of Steel Construction (AISC). Steel Construction Manual, 16th Edition. 2023.
2. McKinsey & Company. Predictive Maintenance and the Future of Industrial Operations. 2022.
3. International Organization for Standardization. ISO 12944: Paints and Varnishes — Corrosion Protection of Steel Structures. 2018.
4. American Welding Society. AWS D1.1/D1.1M: Structural Welding Code — Steel. 2020.
5. U.S. Bureau of Labor Statistics. Occupational Safety and Health Statistics for Fabricated Metal Product Manufacturing. 2022.
6. Engineering News-Record (ENR). Heavy Industrial Construction Trends and Steel Structure Procurement Practices. 2023.
Learn about our latest products and discounts through SMS or email