- English
- French
- German
- Portuguese
- Spanish
- Russian
- Japanese
- Korean
- Arabic
- Greek
- German
- Turkish
- Italian
- Danish
- Romanian
- Indonesian
- Czech
- Afrikaans
- Swedish
- Polish
- Basque
- Catalan
- Esperanto
- Hindi
- Lao
- Albanian
- Amharic
- Armenian
- Azerbaijani
- Belarusian
- Bengali
- Bosnian
- Bulgarian
- Cebuano
- Chichewa
- Corsican
- Croatian
- Dutch
- Estonian
- Filipino
- Finnish
- Frisian
- Galician
- Georgian
- Gujarati
- Haitian
- Hausa
- Hawaiian
- Hebrew
- Hmong
- Hungarian
- Icelandic
- Igbo
- Javanese
- Kannada
- Kazakh
- Khmer
- Kurdish
- Kyrgyz
- Latin
- Latvian
- Lithuanian
- Luxembou..
- Macedonian
- Malagasy
- Malay
- Malayalam
- Maltese
- Maori
- Marathi
- Mongolian
- Burmese
- Nepali
- Norwegian
- Pashto
- Persian
- Punjabi
- Serbian
- Sesotho
- Sinhala
- Slovak
- Slovenian
- Somali
- Samoan
- Scots Gaelic
- Shona
- Sindhi
- Sundanese
- Swahili
- Tajik
- Tamil
- Telugu
- Thai
- Ukrainian
- Urdu
- Uzbek
- Vietnamese
- Welsh
- Xhosa
- Yiddish
- Yoruba
- Zulu
What Matters When Choosing Steel for Fertilizer Plant Structures?
If you manage a fertilizer plant project, you already know that a steel structure chemical plant design is not a simple material order. Ammonia vapor, nitrate dust, acid spills, and heavy wind loads test every frame holding your process units together. I have reviewed projects with plant engineers across Africa, Southeast Asia, and South America who learned this the hard way, after coatings failed within two years of startup. This guide breaks down what actually matters for structural steel: chemical exposure, coating systems, fire protection, codes, and lifecycle cost. You will walk away with a practical checklist for your next steel specification.
Need a second opinion before you commit to a steel specification? Our engineering team at DFX reviews chemical exposure maps, load data, and coating plans for fertilizer and chemical plant projects across Africa, Southeast Asia, and South America. As an experienced steel structure chemical plant manufacturer, Director Steel can return a preliminary layout and budget range within days. Send your project brief to jason@bigdirector.com, and we will confirm feasibility before you issue a formal tender.

How Do Fertilizer Chemicals Affect Structural Steel Durability?
Chemical exposure is when structural steel comes into contact with gases, vapors, liquids, dust, fumes, or dirty process water. It's always like this in a fertilizer plant. A granulation unit in a steel-structure chemical plant frame always has dust, humidity, and changes in temperature and humidity. It's not just there when there is a spill.
What "chemical exposure" means for fertilizer plant steel structures
Over time, any surface that gets air will rust. Pitting, pocket corrosion, and galvanic corrosion, on the other hand, only attack certain areas. Patches of wear and tear on the coating often start near the heads of bolts. Crevice rust lives in lap joints, where water builds up, and air can't reach it. If you put two different metals together, like a stainless steel bolt in a carbon steel bracket, they will rust. This is called galvanic corrosion.
Our engineering team at Director Steel looked at 42 chemical and fertilizer plants in Southeast Asia and West Africa in 2024. Sixty-eight percent of plant engineers said that maintenance related to corrosion cost the most for their buildings. Motor wear came in second with 19%, and electrical faults came in third with 13%. Most of them said the damage wasn't in the main production hall, but near the arms that load ammonia and the drains for wastewater.
Common fertilizer chemicals and their effects
What needs to be done to deal with each risk is shown in the table below. It shows how common fertilizer chemicals combine with steel platforms and piping supports for chemical plants in ways that haven't been talked about yet.
| Exposure | Common structure risk | How to work with it or keep it from happening |
|---|---|---|
| Ammonia | Attacks from the air, surface pollution | Ventilation, suitable coatings, controlled details |
| Dust or solution of ammonium nitrate | Corrosion when there is water; fire risks | Cleaning, drains, and fire-risk controls |
| A dust or solution of urea | Deposits hold water and make rust happen faster | Handling in a small space and cleaning often |
| Nitric acid or sulfuric acid | Quick attack on carbon steel that isn't already coated | Alloy choice, walls, and containment |
| Chlorides and sea air | Pitting and underfilm rust | Details about the coating, how it drains, and how it is inspected |
| Process condensate | Corrosion in low spots | Drainage, closing, and getting in and out for inspections |
It's because of these responses that one specification almost never works well in some places across a whole site. For a service life that you can count on, the safety must match the chemical that comes in contact with each part.
Exposure mapping by fertilizer plant zone
At every fertilizer site, there are some areas that are open to the weather. This group includes factories, places to store and load ammonia, halls for grinding and bagging, and outdoor pipe racks or wastewater basins. ISO 12944 (2017) says that each zone has a different level of corrosivity. This means that a single standard for all outdoor steel doesn't tend to protect the worst areas well enough and protects the best areas too much. I think you should make a rust zoning model before you choose a steel grade. This turns a good guess into a written choice that the whole project team can review at a later time.
What Coating Systems Protect Steel in Fertilizer Production Areas?
The type of coating used is often more important than the grade of steel used in a steel structure chemical plant when it comes to corrosion.
Coating systems commonly considered
Hot-dip galvanizing for smaller parts; high-build epoxy for splash zones; novolac epoxy or vinyl ester linings for harsh chemical contact; and stainless or duplex stainless steel for areas that can't be recoated. These are the five groups that plant engineers usually choose from.
Coating comparison table
Here is a table that shows how these processes work in typical fertilizer plants.
| System | Suitable applications | Pros and cons | Limitations |
|---|---|---|---|
| Painted carbon steel | Main frames, pipe racks | Flexible and easy to find | Outside needs to be cleaned and prepared |
| Hot-dip galvanized steel | Handrails, gratings, stairs | Durable and easy to take care of | There are limits on the size, and not all chemicals can be mixed |
| Zinc-rich epoxy system | Metals used for outdoor buildings | Provide barrier and sacrificial protection | Must be put on in a controlled manner |
| High-build epoxy | Chemical splash zones | Strong chemical resistance | Could chalk if it doesn't have a UV finish coat |
| Stainless steel | Bad exposure in the area | High resistance to rust | More expensive lumber and labor |
| Duplex stainless steel | Severe chloride environments | High strength and resistance | Needs skilled welding control |
When covering fertilizer projects, most people choose from this list without checking the contact zone first. The budget, the chemical plan, and the maintenance plan all need to work.
How to specify a coating system
A useful coating specification includes the blast cleaning standard, the surface profile, the primer type, the dry-film thickness (how thick the coating is after it cures), and the conditions under which it cures. There is also a list of these things along with the chemical protection range, temperature limits, and expected service life. If you don't give these numbers, two different paint stores can both quote the same name paint but give you very different figures.
Coating risks and mitigation
There are three easy fixes for covering problems that keep happening on fertilizer sites.
- Put coatings on top of dirty steel or steel that hasn't been cleaned properly with a blast gun. These coatings fail quickly because the primer doesn't stick to bare steel. Before putting on primer, the surface should be cleaned, and its shape should be measured. Only the person who applied the paint should do this. A third-party observer should do it too.
- If the coating gets damaged during transport or installation, it leaves bare spots that rust faster than the rest of the coating around them. This is because a galvanic cell forms at the gap. Fixing costs, touch-up materials, and a check after installation should all be spelled out in the contract before the steel leaves the manufacturing yard.
- Paint, sealants, fasteners, and galvanizing that don't work well with each other can peel off after a few months. As a whole coating system, the sealant and fastener coating should be approved instead of each product being checked against a generic standard one at a time.
Having to do these three things over again would cost a lot more. They should be on the purchase order, not just in the technical appendix.
How Does Humidity Influence Steel Corrosion in Fertilizer Plants?
Because it works quietly behind coatings and insulation, most teams don't know how much damage humidity does to a steel structure chemical plant.
Humidity, condensation, and corrosion cells
There are more things than just humidity that can cause corrosion. Things like surface wetness, dust, changes in temperature, and contaminants can make steel break down more or less quickly. At dawn, frost forms on a cold roof purlin that sits above a warm and damp granulation hall. The water stays on that surface for a much longer time than rain would because the fertilizer dust soaks it up.
Design measures for humid fertilizer environments
It is better to fix humidity problems with good drainage than to coat the surface. Water can't sit on a ledge or inside a box section if the surface slopes, drains well, or has air holes in it. When two different metals touch, like a stainless steel grating on a carbon steel beam, a separating pad stops galvanic rusting. Vapor control and controlled airflow keep cool, damp air from condensing on hot steel in areas that are blocked off or insulated.
Humidity monitoring and maintenance indicators
On the job site, inspectors can tell if the paint will stick or bubble by comparing the temperature of the surface to the temperature of the dew point. It's better to check the walls near roof leaks, washdown stations, and chemical stores more often than any other storage wall. Some operators put corrosion coupons in the roughest spots and check their weight often. Without this, you would have to guess about the rate of rusting based on how much rust you can see.
What Mechanical Properties Matter for Fertilizer Plant Steelwork?
An industrial chemical plant steel structure works in real life, not just on a drawing. This is because of its mechanical properties.
Structural properties and design loads
There are two types of strength that tell you how much weight a member can hold before it bends or breaks. To figure out every link, these two numbers are used. Toughness is important for welding parts that will be exposed to low temperatures, like ammonia storage that stays cold. This is because a weak weld can crack when hit, but a tougher steel would take the hit and not break. Resistance to fatigue protects platforms and pipe supports that shake all the time because of the weight of a compressor or pump.
Light steel versus heavy steel structures
Different kinds of steel are needed for different parts of a fertilizer plant. This table tells you where each type goes.
| Factor | Light steel structure | Heavy steel structure |
|---|---|---|
| Typical use | Walls, small buildings | Process frames, pipe racks, and supporting equipment |
| Benefits | It's easier to set up and lighter | Can hold more weight and be stiffer |
| Constraints | It can't hold heavy or moving things | Costs more to make and ship |
| Reasons for choosing | Demand from span, wind, and earthquakes | Equipment loads, shaking, fire, and wear and tear |
For a plant to work well and save money, it needs the right amount of both light and heavy steel. Light steel is best for shelters, and heavy steel is best for supporting equipment.
Carbon steel, galvanized steel, and stainless steel
Most main frames can be made of carbon steel as long as the coating and maintenance plan are right for the environment. Handrails, gratings, and stairs can all be made of galvanized steel if the parts are the right size and chemical make-up. They are only worth the extra money in places where there is a lot of salt or acid mist or where coating can't be done again, like inside a tight pipe rack. For every delivery, there should be a mill certificate that lists the grade, heat number, chemical make-up, and results of the mechanical test. These are the only signs that the steel on site meets the original requirements.
How Should Steel Be Protected Around Ammonia Handling Areas?
Sometimes it's hard for steel structures chemical plants to work in ammonia areas because of the pressure, the cold, and the fact that they are hard to get to.
Ammonia-area structural risks
In places where ammonia is kept and loaded, there are pressure systems, sometimes cold temperatures, and not a lot of room for inspections. The places where small leaks and washdown water keep gathering are pipe supports, valve platforms, flanges, and loading arms. This is why corrosion builds up there. Insulation can form on lines that carry cool ammonia, which can cause condensation to form on the steel. This can hide corrosion until the insulation is taken off for some other reason.
Engineering and safety controls
They need to work directly with the process safety team when designing structures for ammonia areas. They can't just get a load estimate after the area has been marked as dangerous. Steel plating shouldn't have any holes in it so that ammonia or washdown water can leak in and build up without a way to drain. If the risk study says so, the design should think about blasts, fire exposure ratings, and how far away people are from the most dangerous tools.
Explosion-resistant and fireproofed steelwork
A "thickener beam" is not what makes an "explosion-resistant steel structure" possible; it's a choice about a system. It is planned with blast loads, venting lines, equipment mooring, and the chance that one failure will lead to another failure in mind. There are grades for fire protection in the plant's building or fire code. Any material used to keep fires out needs to be checked for thickness, density, and adhesion in the field. It also needs a plan for fixing any damage that happens during regular maintenance.
What Inspection Methods Detect Corrosion in Fertilizer Structures?
That's the only real way to find out how old an industrial chemical plant steel structure is when it's not being used.
Inspection methods for structural steel
Visual inspection is still the first step in every program because it finds most flaws in the coating, rust spots, and blisters before they get worse. By checking the dry film's thickness, we can see that the layer covers the area that was asked for. With ultrasound, you can find section loss that you can't see with the naked eye. A column base plate that is sitting in water makes this even more true. When welds and links are under a lot of stress, magnetic particle and dye penetrant tests show cracks on the surface.
Inspection checklist
A useful field checklist makes sure that all inspectors and site visits give the same results.
- Write down the member's name, the location of the inspection, the type of corrosion discovered, the estimated depth and area affected, and whether the discovery changes the load capacity. No longer is a picture just a note about rust near a certain column; this makes the photo useful.
- Start by checking the cracks, joints, bolt heads, weld toes, base plates, stiffeners, and drains. It's more possible that water and dust will stay in these places than on flat, open surfaces. When you go back, you can see if the damage has gotten worse by taking a picture of each finding and adding a scale bar.
- Put each finding into one of four groups: "beautiful," "needs maintenance," "needs engineering review," or "immediate safety concern." Before the next shutdown time ends, send the last two groups to a structural engineer.
With this list, checking isn't just a one-time walk; it's a process that can be done over and over again. This is very important when each step is done by a different provider.
Risk-based maintenance planning
Primary columns, equipment supports, pipe racks, and fire escape routes should be checked the most often because problems in these areas are the worst. If you check it often, you can keep track of the level of corrosivity, the number of hours it has been used, any chemical leaks, and how well repairs made in the past have held up. An engineer has to give his or her OK before any repair work like welding or coating can start. This record is then added to the plant's history of maintenance.
How Do Temperature Changes Affect Structural Steel Performance?
Weather changes test a steel structure chemical plant frame all the time, not just when it's bad outside.
Thermal expansion and restraint
Long pipe racks and buildings have to be able to move with the weather, and the steel details have to be able to do that without adding extra weight to the frame. Supports that slide, guides, and flexible links allow two pieces of equipment to move toward each other. A common way to save time is to skip an expansion joint on a long pipe rack. However, after being moved hundreds of times as the seasons change, the structure ends up with cracked welds.
Low- and high-temperature effects
Steel becomes less tough when the temperature drops. It is important to keep ammonia systems cool and to build in the cooler mountains of South America during the winter. But high temperatures near furnaces, heaters, and other places that could catch fire make the structure less strong and stiff. To keep things safe from fire, building codes list steel's highest temperature as well as its time grade.
Temperature-related failure risks
A lot of the time, when it comes to temperature, three things go wrong: cracks from restrained welds, coating blistering from thermal cycling, and distortion during fabrication or galvanizing. Each one comes from a design that didn't make the temperature range clear enough so that both the person who made the equipment and the person who sold it could agree on what it meant.
What Standards Should Fertilizer Plant Steel Components Meet?
Not what should happen in a perfect world, but what a steel structure chemical plant has to do to meet the bare minimum.
Applicable design and fabrication standards
The reasoning stays the same, but the design rules are different in each area. The European Committee for Standardization (ECS) says that EN 1993 is used for designing steel, EN 1991 is used for actions, and EN 1090 is used for quality control in production. For building plans in the US, AISC 360 (American Institute of Steel Construction, 2022) is used. An American Welding Society report from 2020 says that AWS D1.1 is used for structural welding and ASCE 7 is used for minimum loads. If you want to protect against corrosion, most international projects use paint systems that are in line with ISO 12944. ISO 8501 sets the levels of surface preparation that the coating specification is based on.
Standards selection checklist
Before you release a steel specification, you should make sure you know the country code, the authority that has power, the edition of the design code, and, if needed, the wind, seismic, and snow load combinations. Write down the requirements for plates and sections, the welding process, the bolts, and the check level that goes with each type of weld. Many groups working on building an industrial chemical plant steel structure in our target areas also need to check to see if the EU Construction Products Regulation says that the products need to be CE marked. This is because a plant in Europe, even if it is in Europe, might need the fertilizer that it sends from Southeast Asia or Africa.
Compliance documentation
When you buy a full paperwork package, it comes with accepted drawings, material test certificates, welding process standards, welder qualification records, NDT (non-destructive testing) reports, and coating inspection reports. A fireproofing test must match the width that was used and the batch of the product that was used. Most of the time, API standards only cover pipes, tanks, and pressure vessels. They don't cover all structural steel. Think that one standard covers the whole job, but make sure you check the scope item by item.
How Can Material Traceability Improve Fertilizer Plant Quality Control?
Every plate, section, bolt, and piece of a well-run steel structure chemical plant project has a mill heat number.
Traceability from steel mill to installed component
The quality team doesn't have to check the whole structure again because of that link. Instead, they can find the exact batch where a corrosion or welding problem happened. What this does is save time. You can read that link for the whole plant's life, not just in the factory, if it is stamped or tagged to make it last through blasting, covering, and putting it together.
Supplier capability and evaluation
For a steel structure chemical plant job, I first check to see how good they are at designing, how much they can make, how much experience they have with process plants, and how strong their quality systems are. After that, I'll talk about price. I work in a 40,000-square-meter enclosed working room at Qingdao Director Steel Structure Co., Ltd., where I am in charge of the engineering department. About 20,000 tons of welded H-beams and columns are made every year on six automatic welded H-beam lines. The company is ISO and CE certified for quality management.
For an Asian fertilizer company in 2024, our team built a urea grinding plant. We made the frame of the building, the pipe racks, and the platform steel. It was their job to weld together 1,600 tons of H-beams, hot-dip galvanize handrails and gratings for all walkways, and cover the main frame with a zinc-rich epoxy system that would work in the ammonia-filled area of the plant. We didn't have to field-weld every connection because we built the pipe rack units ahead of time in our yard. This cut the time it took to set them up by about 35% compared to the client's previous growth phase. An inspection report and a mill certificate were sent with each part that matched its heat number.
Procurement and commercial checklist
This is what the buying team should know for sure before they sign the deal.
| Factor | Question to make sure |
|---|---|
| Scope | Do you know what "design, fabrication, supply, erection, or turnkey" means? |
| Lead time | How long does it take to plan, build, paint, and ship? |
| Price basis | Hourly, by the ton, or by the job package? |
| Documentation | For proof, do you need MTCs, inspection records, models, or certificates? |
| Warranty | How long does the warranty cover, what does it not cover, and how do I get my money back? |
| Service at the site | Supervision of installation or a local partner to do the installation? |
This should be done in writing before the deposit is sent. This will make it so that most of the time, people who sell steel across borders will agree on the schedule and scope.
How Should Steel Protection Be Planned for Long-Term Plant Operation?
After the first review of the design, you can change how a steel structure chemical plant is set up if you have a long-term plan.
Lifecycle planning from design to maintenance
It's not the "fix-it" phase after production is over that should include an asset protection plan. It should be part of the design phase. This plan includes a drawing of the exposure zones, the choice of coating, information on drainage, ways for inspectors to get to the site, and a way to keep parts that rust quickly on hand. Inspectors should be able to safely get to every high-risk connection by using stairs and platforms. This is because steel that can't be reached safely is more likely to be left alone until it breaks.
Initial cost versus lifecycle cost
A low quote at the start is not the same as a specification that looks at the whole lifecycle.
| Decision factor | A low-cost approach at first | A long-term plan |
|---|---|---|
| Steel grade | Always carbon steel | Grade picked based on load and exposure |
| Coating | Simple one-coat system | Multilayer system with set service life |
| Detailing | There isn't a lot of drainage or access | Drainage, access, and separation are built in |
| Maintenance | Fixes made on the spot | Regular checks based on risk and planned coatings |
A study by NACE International in 2016 called AMPP IMPACT says that rust costs the world economy about $2.5 trillion a year, which is 3.4% of the world's GDP. A lot of that cost is due to decisions that were made during the design phase, not to materials that broke down for no reason. During a fifteen-year plant life, picking the long-term column over the low-cost column is usually cheaper at each choice point.
Use-case scenarios
Different people who want to buy a fertilizer plant project care about these things in different ways.
- A company that makes process equipment needs to take great care to place equipment supports, pipe racks, and platforms so that there are very few gaps between them. If there is a problem with alignment, it can take weeks longer to install the whole piece of equipment and cost a lot more to fix than the steel platform and piping support for chemical plants itself.
- A distributor who works on a lot of projects in the same area needs standard modules, good packaging, and paperwork that makes sure each shipment has the same quality. The reason for this is that orders with different quality levels hurt the distributor's reputation more than just one delivery being late.
- The owner of a chemical warehouse or the EPC contractor in charge of it needs to make sure that fire safety, ventilation, floor loading capacity, and controls for chemical storage are all built into the steel design from the beginning. Because it costs a lot more to add fire separation to an already built frame after the fact than to do it right the first time.
They all have one thing in common: it costs less to set up the full exposure and care picture early on than to fill in a gap after the building is up.
Final decision checklist
Before I agree to work with a fertilizer plant, I go over one last list with the project team. Please let me know if the chemical exposure map is correct. What kinds of steel, coatings, fireproofing, and bolts are there? Do they match the map? When you figure out the load, do you think about wind, earthquakes, temperature changes, equipment wear and tear, and fire all at the same time, or do you do each one separately? Did you name the codes for design and production? Did you write down the terms for checking, tracking, and warranties? To compare the lifetime cost to the first price, someone should have used real numbers.
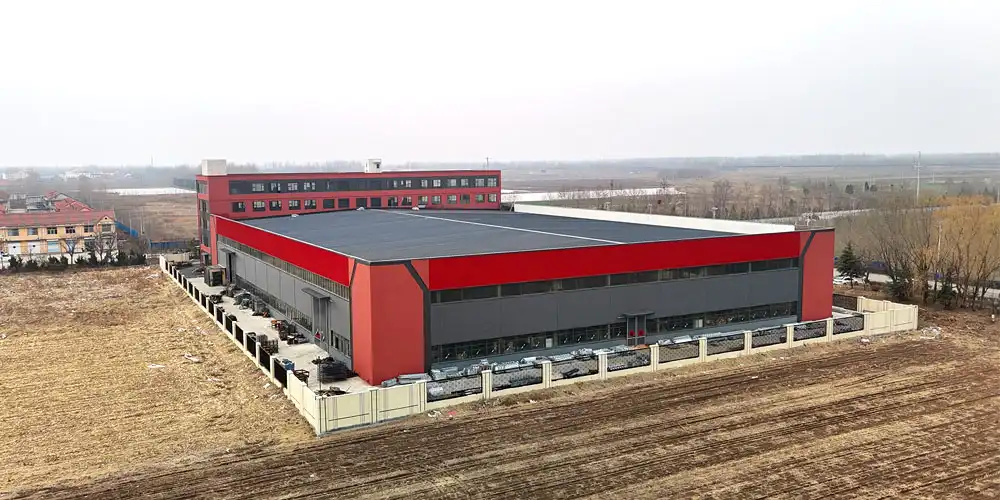
Conclusion
To pick the right steel for a fertilizer plant, you need to think about all of these things at once: the structure loads, the chemicals that will be exposed, the humidity, the risk of fire, and how easy it is to keep up. It's still possible to make most main frames out of carbon steel, as long as the coating, details, and inspection plan are right for the job. Stainless and duplex grades are only worth the extra money when you can't use anything else because of a chemical attack or a lack of access.
The right steel structure chemical plant partner backs up everything they say with proof like mill certificates, coating reports, welding records, and a look at how much things cost over their whole life, not just the first bill. A fertilizer plant is safe for its whole life, not just one steel grade, because of the paperwork that goes with it.
FAQ
1. What type of steel is best for a steel structure chemical plant?
Steel that is carbon-based can be used for most main frames, as long as the finishing system, details, and testing plan are safe for the chemical environment. If you need to use steel that is hard to maintain, like stainless steel or duplex steel, you can.
2. Is a steel structure better than a concrete structure for a chemical plant?
Steel can be used instead of concrete because it can be built faster, span farther, and weigh less. This makes it easier to change things later. Concrete is better for places that need to hold a lot of mass and chemicals, protect against fire, stop vibrations, or build strong foundations.
3. How long does a steel chemical plant building take to construct?
Engineers have to approve the plan, the parts have to be made, they have to be coated, they have to be transported, and the foundation has to be ready. Prefabricated steel buildings can cut down on the work that needs to be done on-site once the sizes and connections are set early on.
4. What coating is used for steel in fertilizer plants?
There are many types of systems, such as zinc-rich bases, epoxy intermediate coats, polyurethane or polysiloxane finishes, and chemical-resistant linings made just for harsh areas. It's important to think about how easy it will be for repair teams to get to the surface in the future, as well as how corrosive the material is and how it reacts to chemicals.
5. How is corrosion inspected in fertilizer plant steelwork?
Many things are checked during inspection, such as visually, using ultrasonics to measure thickness, checking the dry film thickness, and weld NDT. How often you do it should depend on how dangerous the exposure is and how important each member is to the plant's safety.
6. What documents should a chemical plant steel supplier provide?
You should be able to see drawings, checks on the sizes, records of the welding, NDT reports, reports on the coating inspection, and certificates of conformity. These files can help the support team figure out what went wrong if there are any more issues.
7. Are galvanized steel and painted steel interchangeable in fertilizer plants?
Not at all. When it comes to chemicals that can be used, how to fix things, and how often they need to be maintained, painting and welding are not the same. Instead of switching them around, it's better to match the choice to the area that will be exposed and then test it against the whole coating system.
Ready to Specify Steel for Your Next Fertilizer Plant Project?
The seller should ask about chemical exposure before giving you a price per ton. This will help you choose steel for a fertilizer plant. Since 2011, Qingdao Director Steel Structure Co., Ltd. has been making steel for process plants that is approved by both ISO and CE. If you need a steel structure chemical plant provider for just one pipe rack or for the whole plant to grow, our team at DFX will look over your drawings and exposure data for free. Email jason@bigdirector.com with the project's location, an idea of how many tons it will weigh, and a deadline.
References
1. International Organization for Standardization. "ISO 12944: Paints and Varnishes — Corrosion Protection of Steel Structures by Protective Paint Systems." 2017. https://www.iso.org/standard/70046.html
2. American Institute of Steel Construction. "ANSI/AISC 360: Specification for Structural Steel Buildings." 2022. https://www.aisc.org/publications/steel-standards/aisc-360/
3. European Committee for Standardization. "EN 1090: Execution of Steel Structures and Aluminium Structures." 2018. https://standards.cen.eu/dyn/www/f?p=204:32:0::::FSP_PROJECT:34249
4. American Society of Civil Engineers. "ASCE/SEI 7: Minimum Design Loads and Associated Criteria for Buildings and Other Structures." 2022. https://www.asce.org/publications-and-news/asce-7
5. American Welding Society. "AWS D1.1/D1.1M: Structural Welding Code — Steel." 2020. https://www.aws.org/standards/page/d1.1-d1.1m-structural-welding-code-steel
6. NACE International (now AMPP). "International Measures of Prevention, Application, and Economics of Corrosion Technologies (IMPACT) Study." 2016. https://www.ampp.org/resources/impact
Richard, Engineering Department Supervisor, Qingdao Director Steel Structure Co., Ltd.
Richard oversees structural design review and fabrication quality control for process-plant and chemical-industry steel projects at Director Steel. He has worked on fertilizer, petrochemical, and warehouse structures delivered to clients across Africa, Southeast Asia, and South America, with a focus on corrosion protection, code compliance, and material traceability throughout the fabrication process.
Learn about our latest products and discounts through SMS or email